Master the fundamentals of sheet metal stamping with this full engineering guide covering processes, tooling dies, DFM rules, materials, tolerances, and production cost factors. Contact Precintl today for instant DFM analysis and scalable OEM / ODM contract manufacturing.
High-volume hardware manufacturing depends on fast, repeatable, and structurally sound cold-forming operations. Whether you are engineering a custom enclosure, automotive structural bracket, or micro-connector shield, selecting the right cold-forming strategy determines your unit economics and dimensional stability.
At its core, sheet metal stamping converts flat sheet metal blanks into defined 3D shapes through mechanical or hydraulic presses equipped with custom die sets.
What Is Sheet Metal Stamping?
Understanding how cold forming compares to alternative manufacturing methods helps product teams select the right process early in the design cycle.
How Sheet Metal Stamping Works
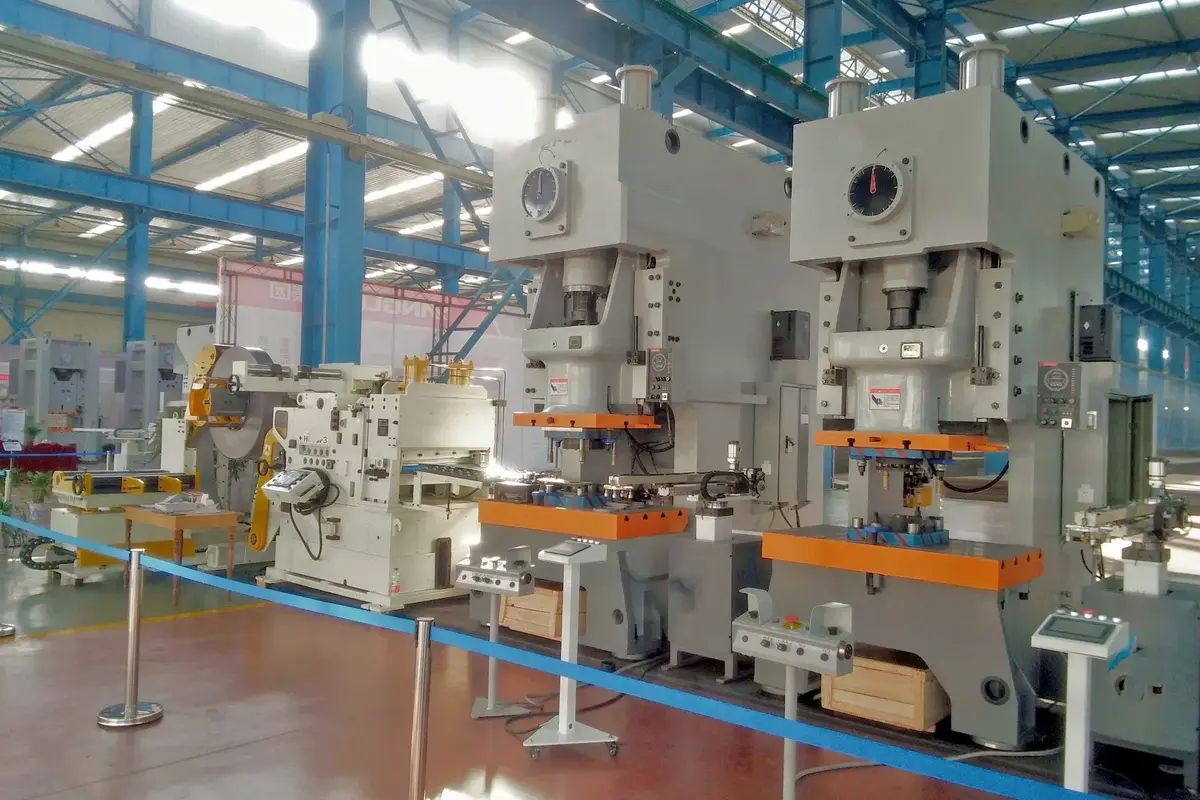
The cold-forming press applies high mechanical force to shear, bend, or draw raw sheet metal stock clamped between die sections. Upper punches descend into matching lower cavity dies, exceeding the material’s yield strength to induce permanent deformation without melting or machining away stock.
What Types of Parts Can Be Made With Stamping?
Engineers specify this process for parts requiring thin walls, high structural rigidity, and intricate contours. From EMI shields to chassis brackets, metal parts stamping provides rapid replication across brackets, spring clips, terminals, motor laminations, deep cups, and structural automotive panels.
Sheet Metal Stamping vs. Metal Stamping
While industry terminology often overlaps, metal stamping serves as a broad umbrella term covering all press operations on metallic alloys. By contrast, sheet metal stamping specifically denotes operations performed on thin flat sheets or coiled strip stock, typically ranging from 0.2 mm to 6.0 mm in thickness.
How the Sheet Metal Stamping Process Works
Executing a high-yield sheet metal stamping run depends on systematic planning long before raw coil stock reaches the press floor.
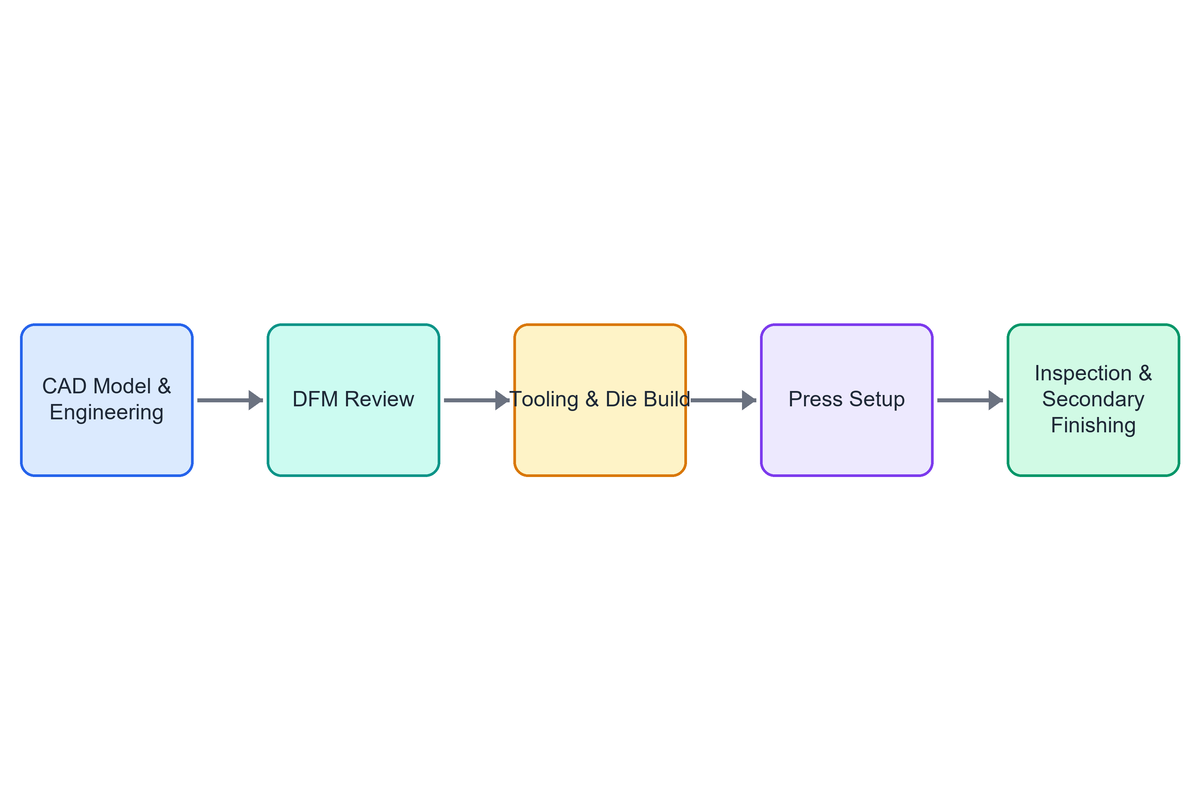
Part Design and DFM Review
Every custom sheet metal stamping project starts with thorough engineering evaluation. Designers evaluate material elongation properties, bend radii, hole clearances, and grain direction to prevent thinning or shear failure during press cycles.
Material and Sheet Thickness Selection
Selecting material thickness involves balancing mechanical load demands against press tonnage limits. Thicker gauges require higher press capacity and larger bend radii, while thinner gauges demand strict handling to avoid oil-canning and edge buckling.
Stamping Die Design and Tooling
Tooling engineers craft precision die sets using hardened tool steels. Dies incorporate punches, die plates, guide pillars, strippers, and spring nitrogen pads designed to absorb hundreds of thousands of press strokes without dimensional drift.
Blanking, Piercing and Cutting
The process begins by shearing raw coil stock. Blanking cuts the outer profile away from the primary coil, whereas piercing punches internal holes, slots, and notches into the workpiece.
Bending, Forming and Drawing
Once blanked, internal stations bend features along linear axes or draw sheet material into deep hollow pockets. Form punches force the sheet into die cavities, maintaining tight angular control through pre-calculated springback allowances.
Secondary Operations and Finishing
Post-press operations address functional and cosmetic requirements. Parts undergo deburring, ultrasonic cleaning, heat treating, plating, powder coating, or inserting captive fasteners (PEMS) for downstream assembly integration.
Inspection and Production Validation
Quality technicians verify critical dimensions using optical comparators, coordinate measuring machines (CMM), and automated vision systems during tool setup and active production runs.
Related: PCB Design: Complete Guide to PCB Layout, DFM, Manufacturing & Assembly
Types of Sheet Metal Stamping
Choosing the correct die configuration balances initial tooling investment against unit cycle speed.
| Die Type | Key Characteristics |
|---|---|
| Progressive | Continuous / High-Speed |
| Transfer Die | Independent Stations |
| Compound Die | Single-Pass Cut & Form |
| Deep Draw | Cupped / Hollow Geometry |
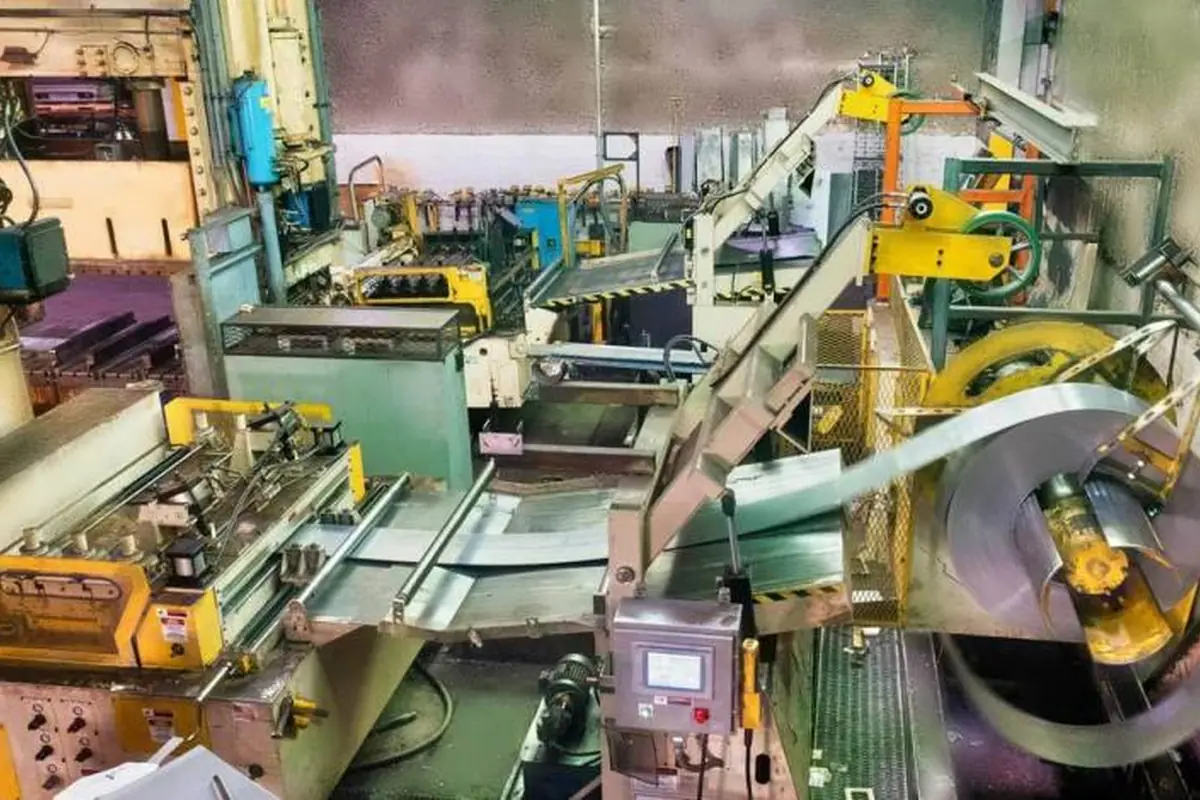
Progressive Die Stamping
In progressive die stamping, a continuous coil feeds through consecutive workstations. Each press stroke performs cutting, punching, or forming steps simultaneously before the finished component detaches at the final station.
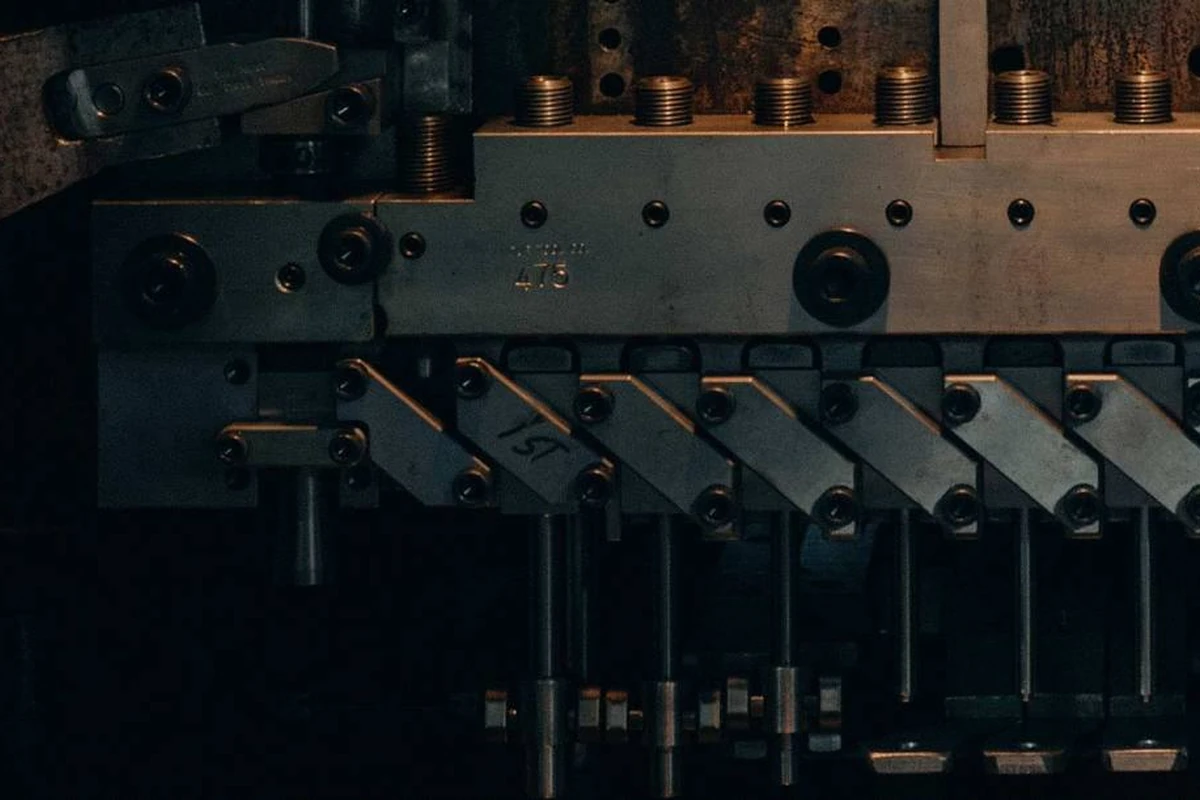
Transfer Die Stamping
For large structural components, transfer die stamping moves discrete parts between standalone die sets using mechanical fingers. This setup suits bulky automotive body panels and heavy industrial enclosures that cannot remain attached to a continuous strip.
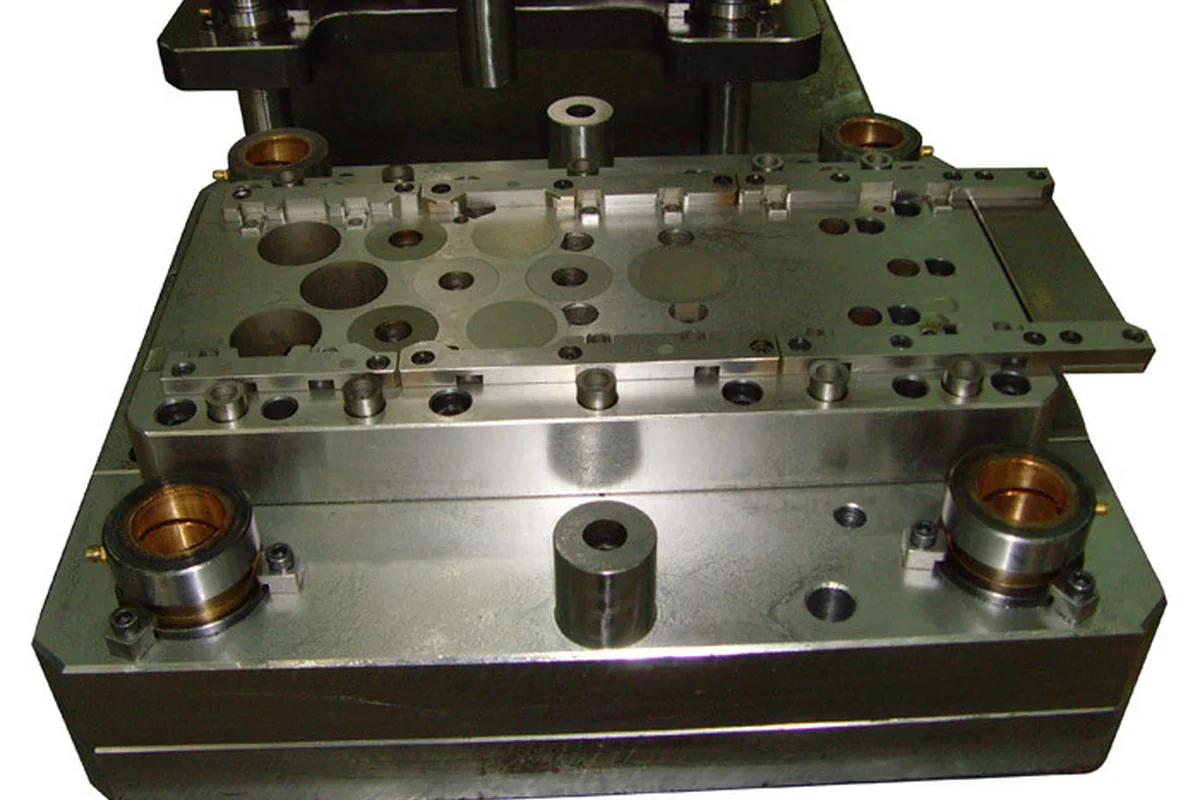
Compound Die Stamping
Compound dies execute multiple cutting operations—such as outer blanking and inner piercing—in a single press stroke. This approach delivers outstanding concentricity and edge-to-hole accuracy for flat parts like washers, shims, and motor laminations.
Deep Draw Stamping
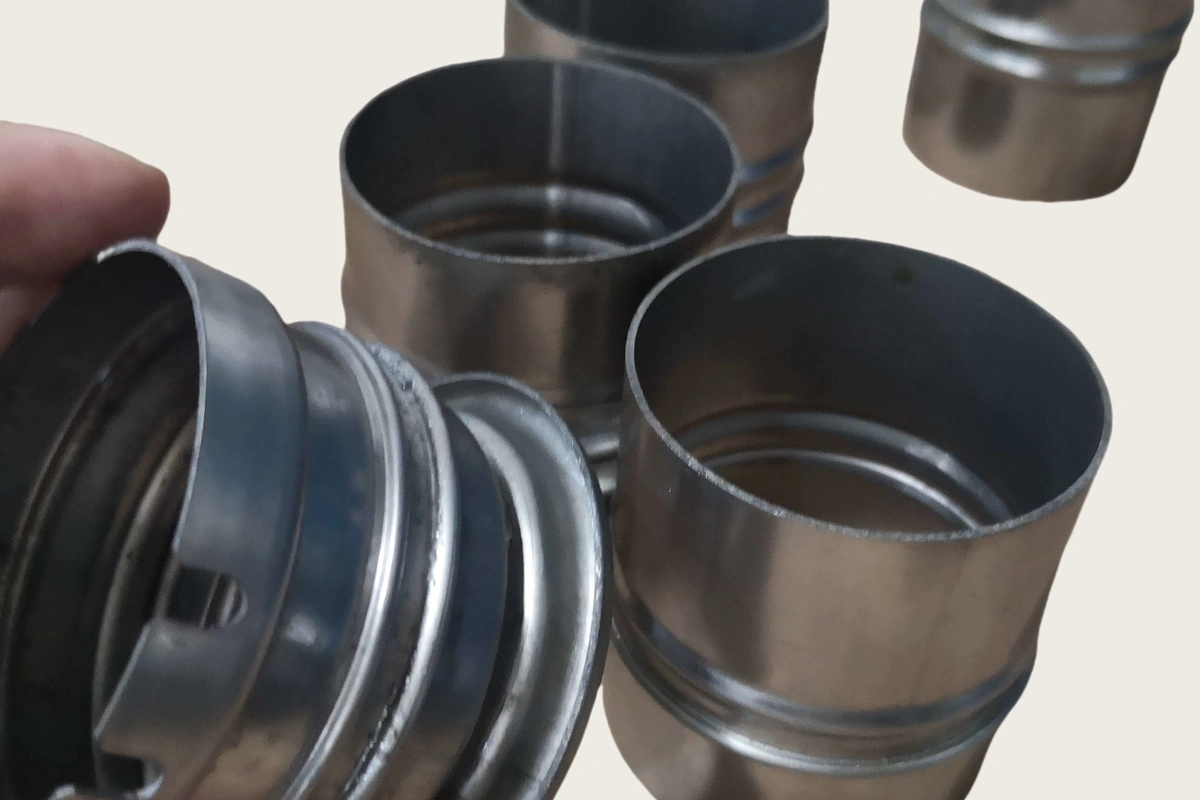
When part depth exceeds its diameter, deep draw stamping stretches the blank into seamless cylindrical or rectangular shapes. A holding punch restrains material flow to yield uniform wall thickness without tensile rupture.
Fineblanking
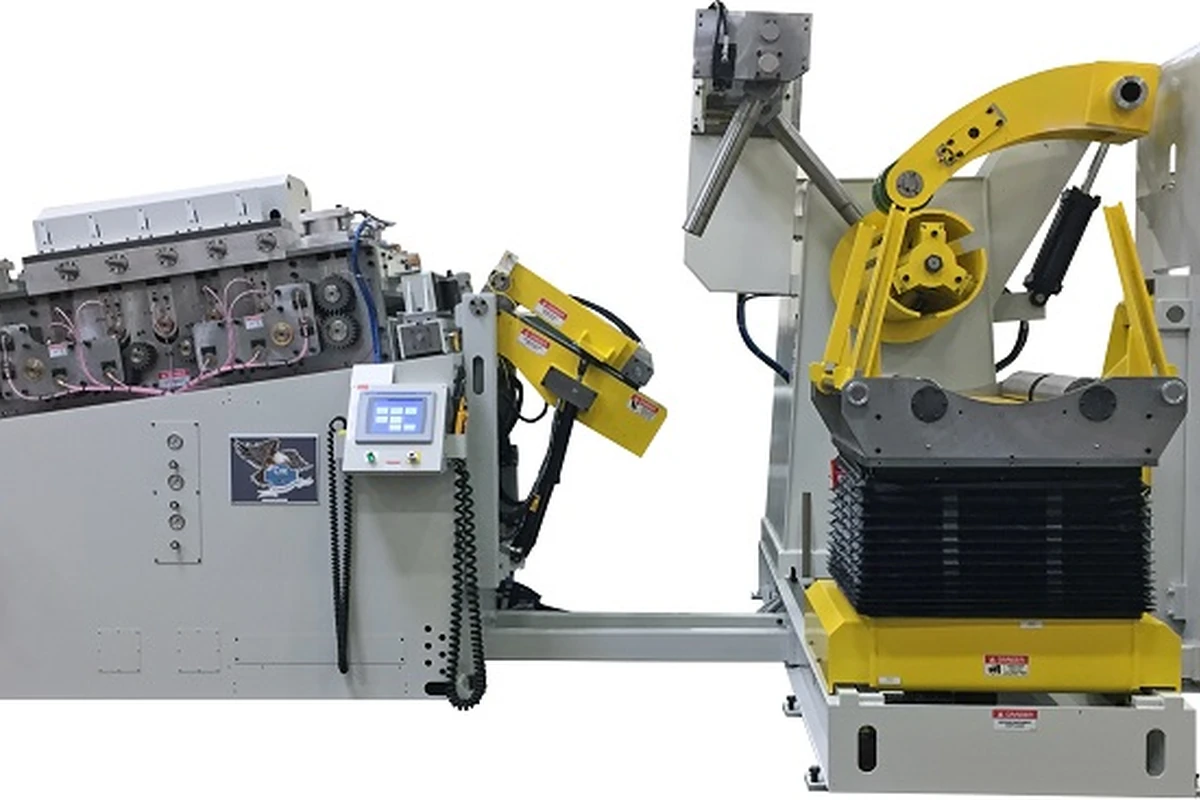
Fineblanking combines high clamping pressure with minimal die clearance to produce completely shear-burnished edges without burrs or tear zones. It eliminates secondary reaming for gears and latch mechanisms.
Single-Operation Stamping
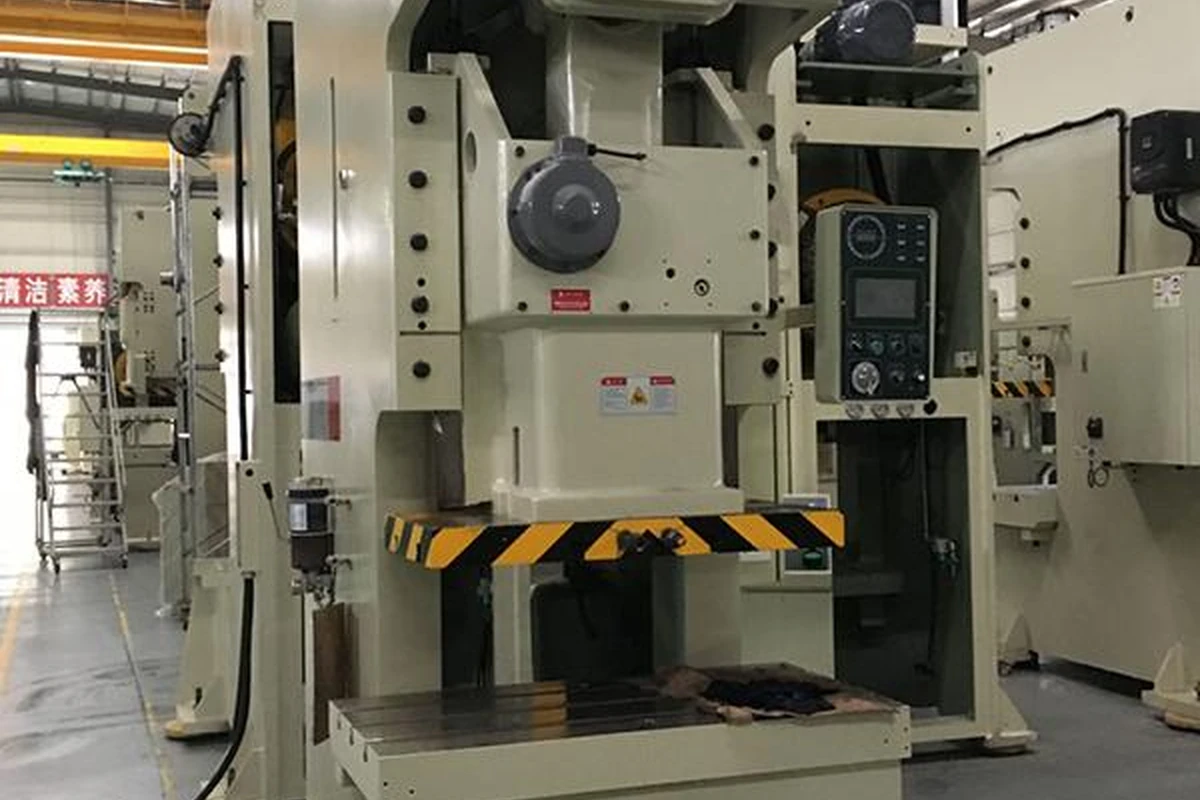
Low-volume runs often rely on stage tooling where operators manually transfer blanks between dedicated presses for individual shearing, bending, or punching operations.
Materials Used for Sheet Metal Stamping
Selecting suitable sheet metal stamping materials directly impacts tool wear, springback behavior, and corrosion performance.
| Material Family | Common Grades | Key Advantages | Typical Applications |
| Stainless Steel | 304, 316, 430 | Superior corrosion resistance, high tensile strength | Medical devices, food equipment, exterior brackets |
| Carbon & Mild Steel | SPCC, SECC, 1018 | Excellent formability, cost efficiency, high strength | Automotive frames, structural brackets, heavy machinery |
| Aluminum | 5052, 6061-T6, 1100 | Lightweight, non-magnetic, natural oxide layer | Electronics shields, aerospace panels, heatsinks |
| Copper | C11000, C10200 | Exceptional electrical and thermal conductivity | EMI shielding, busbars, electrical contacts |
| Brass | C26000, C26800 | Smooth low-friction wear, attractive gold finish | Decorative trim, fluid fittings, lock components |
Stainless Steel
Stainless alloys deliver robust strength and environmental resistance. Austenitic grades (304, 316) offer excellent formability but exhibit noticeable work hardening, requiring heavy-duty press tonnage and wear-resistant tool coatings.
Carbon and Mild Steel
Cold-rolled carbon steels serve as workhorses for industrial components. Cold-rolled grades feature tight thickness tolerances and smooth surface finishes ideal for structural brackets receiving secondary paint or zinc plating.
Aluminum
When lightweight strength is required, aluminum stamping provides excellent strength-to-weight ratios. Alloys like 5052 offer high ductility for sharp bends, while heat-treatable 6061 requires careful radius planning to avoid grain cracking.
Copper
Pure coppers offer low electrical resistance for high-current applications. Because annealed copper is soft, tooling must incorporate polished surfaces to prevent galling during drawing and punching.
Brass
Brass alloys combine mechanical strength with natural lubricity and corrosion resistance. They form easily without rapidly galling tool steel surfaces.
How to Select the Right Stamping Material
Evaluate operating environment, electrical conductivity needs, structural load requirements, and target yield strength. Match material ductility to draw depths to keep tooling costs low.
Related: Compression Molding: Process, Materials, Types, Benefits, Applications & Cost Guide
Sheet Metal Stamping Design Guidelines
Adhering to standard sheet metal stamping design guidelines prevents premature cracking and tool breakage while keeping unit costs predictable.
Material Thickness and Formability
Keep wall thickness uniform across the part geometry. Sudden thickness variations create localized stress concentrations and uneven material flow during press closure.
Bend Radius and Bend Allowance
Specify an inside bend radius equal to or greater than the stock thickness (R >= 1.0 * t). Bending sharp internal radii tears outer metal fibers and causes premature fatigue failures.
Hole Size and Feature Placement
Ensure hole diameters equal or exceed sheet thickness (D >= 1.0 * t). Maintain a minimum spacing of 2.0 * t between hole edges and bend lines to prevent oval deformation during forming.
Tolerances and Dimensional Requirements
Avoid unnecessarily tight tolerances on unformed features. Standard commercial tolerances keep production moving smoothly; reserved precision zones should be designated only for critical mating interfaces.
Grain Direction and Part Orientation
Orient primary bend lines perpendicular (90°) or diagonally (45°) to the raw material rolling grain direction. Bending parallel to the grain increases cracking risks along the bend outer radius.
Burr, Edge and Surface Requirements
Punching operations create natural burrs on the die side of the sheet, typically running 5% to 10% of sheet thickness. Clearly note burr-side requirements on engineering drawings so tooling designers position punches correctly.
Designing Parts for Manufacturability
Integrating early sheet metal stamping DFM feedback eliminates narrow web gaps, complex cutouts, and tight internal cut corners that weaken progressive punches.
Sheet Metal Stamping Dies and Tooling
Investing in high-grade sheet metal stamping tooling lowers total long-term unit costs across high-volume production cycles.
How Stamping Dies Are Designed
Tool designers utilize 3D CAD software and FEA simulation to model metal flow, press force vectors, and springback behavior. Dies incorporate modular carbide or hardened tool steel inserts for simplified maintenance.
Custom Die Manufacturing
Toolmakers fabricate precision components using wire EDM, CNC milling, surface grinding, and vacuum heat treatment. Custom die manufacturing requires exacting tolerances to ensure proper punch-to-die clearances.
Die Testing and Process Validation
Before release to active production lines, die sets undergo rigorous trial tryouts. Quality engineers run test strips to check dimensions, burr heights, material feed pitch, and springback recovery.
Tool Maintenance and Expected Die Life
Routine sharpening, polishing, and lubrication extend die longevity. High-quality tool steel dies typically execute between 500,000 and 2,000,000 press strokes over their usable lifespan.
Sheet Metal Stamping Tolerances and Quality Control
Standard sheet metal stamping tolerances typically range between +/-0.05 mm and +/-0.2 mm depending on feature type, material gauge, and press stability.
| Tolerance Type | Range | Note |
|---|---|---|
| Standard Tolerances | +/- 0.10 mm to +/- 0.20 mm | Cost Effective |
| Precision Tolerances | +/- 0.02 mm to +/- 0.05 mm | Requires Fineblanking / Secondary Checks |
What Determines Stamping Accuracy?
Tolerance stability depends on press deflection, sheet thickness consistency, lubricant viscosity, die temperature, and punch wear rates over extended production runs.
Dimensional and Visual Inspection
Operators perform periodic statistical process control (SPC) checks using plug gauges, micrometers, height gauges, and visual inspection plates.
Common Quality Control Methods
Automated vision systems inspect fast-moving progressive strips for missing holes or burrs. CMM equipment creates 3D point-cloud models to verify complex drawn contours against CAD files.
Managing Tight-Tolerance Stamped Components
For complex enclosures with sub-millimeter features, precision sheet metal stamping delivers exact geometric control through tight-clearance tooling and automated temperature-controlled press bays.
Common Sheet Metal Stamping Defects and How to Prevent Them
Recognizing defect root causes allows shop-floor technicians to adjust press settings before parts fall out of spec.
| Defect Type | Primary Root Cause | Actionable Shop-Floor Solution |
|---|---|---|
| Cracking & Tearing | Exceeded material elongation limit | Increase bend radius; check grain |
| Wrinkling | Insufficient blank holder pressure | Increase nitrogen spring force |
| Excessive Burrs | Dull punches or wide die gap | Resharpen punches; re-align die |
| Springback Drift | Elastic elastic recovery | Add ribbing; apply over-bending |
| Surface Scratches | Die galling or debris | Polish dies; improve lubrication |
Related: Drop Forging: Process, Types, Materials, Benefits, Applications & Cost Guide
Cracking and Tearing
Tensile failure occurs when material stretch exceeds yield limits. Solution: Increase punch corner radii, apply specialized press lubricants, or switch to an annealed alloy state.
Wrinkling and Buckling
Compressive forces cause excess sheet metal to fold or wave in deep draw zones. Solution: Increase blank holder pressure to clamp the stock securely during draw strokes.
Burr Formation
Excessive burrs form when punch-to-die clearances widen from wear. Solution: Maintain proper shear clearance (typically 5-10% of material thickness) and schedule regular punch resharpening.
Springback
Metals naturally spring back slightly after the press punch retracts. Solution: Design dies with deliberate over-bending angles or introduce stiffening ribs along bend lines to lock geometry in place.
Dimensional Inconsistency
Pitch variations along progressive strips lead to wandering feature placement. Solution: Install hardened pilot pins inside the die to fix strip positioning before punches make contact.
Surface Damage and Deformation
Galling and particle pickup mar part appearance during metal-on-metal sliding. Solution: Apply TiN or TD coatings to punches and implement continuous coil cleaning brushes.
Benefits of Sheet Metal Stamping for Production
Because cycle times are measured in milliseconds, sheet metal stamping for mass production offers unbeatable unit economics.
High-Volume Production Efficiency
Modern press suites operate at speeds ranging from 30 to over 500 strokes per minute, generating thousands of finished components per hour.
Consistent Part Repeatability
Hardened tool steel dies eliminate human variability, delivering identical part dimensions across hundreds of thousands of production units.
Reduced Per-Part Manufacturing Cost
Although initial die fabrication requires upfront investment, high unit volumes dilute tooling expenses to fractions of a cent per component.
Complex Features in a Single Production Process
Progressive tooling combines piercing, lancing, coin-stamping, embossing, and forming into a unified press stroke line.
Material Utilization and Production Optimization
Engineers layout nesting patterns along raw coil stock to optimize yield, minimizing scrap generation and lowering raw material spend.
Sheet Metal Stamping Applications Across Industries
Hardware components produced via cold press operations serve as structural backbones in nearly every modern engineering sector.
Consumer Electronics and Smart Devices
Ultra-thin internal frames, antenna clips, and heat-sink plates utilize custom metal stamping to fit compact device enclosures.
Electrical and Electronic Components
High-precision sheet metal stamping for electronics produces intricate connector pins, busbars, lead frames, and shield cans with silver or tin plating.
Automotive Components
Heavy-duty structural brackets and body panels rely on sheet metal stamping for automotive parts where high-tensile steels protect passenger cabins.
Industrial Equipment and Machinery
Thick-gauge steel plates, motor mounting brackets, and electrical panel enclosures handle heavy mechanical loads under demanding environments.
Smart Home and IoT Products
Sleek metal trims, internal mounting plates, and spring battery terminals keep smart home hubs compact and easy to assemble.
Medical and Healthcare Equipment
Passivated stainless steel components provide corrosion resistance for diagnostic devices, surgical tool handles, and pump housings.
Hardware, Brackets and Enclosures
Simple L-brackets, structural gussets, and DIN-rail clips form the building blocks of modular cabinet installations.
Sheet Metal Stamping vs. Other Manufacturing Methods
Selecting the correct process requires evaluating production volumes against upfront tooling lead times.
| Feature / Process | Sheet Metal Stamping | CNC Machining | Laser Cutting | Die Casting |
|---|---|---|---|---|
| Optimal Volume | High (> 5,000 pcs) | Low to Medium | Low to Medium | High (> 5,000 pcs) |
| Unit Cycle Time | Seconds | Minutes to Hours | Minutes | Seconds |
| Upfront Tooling Cost | Moderate to High | Low / None | Low / None | High |
| Material Scrap | Low (Optimized Nest) | High (Subtractive) | Moderate | Low |
| 3D Geometric Depth | Good (Deep Draw) | Exceptional | Flat / 2D Only | Exceptional |
Stamping vs. CNC Machining
Machining carves parts out of solid blocks, creating significant material waste and slow cycle times. Stamping forms thin sheet stock in seconds without material removal.
Stamping vs. Laser Cutting
Laser cutting requires zero hard tooling, making it ideal for low-volume prototypes. However, once volumes exceed several thousand units, stamping’s rapid stroke speed yields lower unit costs.
Stamping vs. Sheet Metal Fabrication
Manual press brake folding and punching suits custom low-volume runs. Stamping replaces manual labor with automated progressive dies for mass production.
Stamping vs. Die Casting
Die casting injects molten metal into mold cavities, creating complex thick-walled parts. Stamping relies on cold working thin sheet metals, yielding lighter parts with higher tensile strength.
When Should You Choose Stamping?
Choose cold press operations when your annual production volume exceeds 5,000 units, part geometry uses uniform wall thickness, and rapid unit production is mandatory.
Related: EMS Electronic Manufacturing Explained: From Design to Mass Production (2026)
How Much Does Sheet Metal Stamping Cost?
Calculating the total sheet metal stamping cost involves balancing initial tooling outlay against unit volume targets.
Material and Sheet Metal Costs
Raw coil stock represents a primary ongoing expense. Selecting common commercial grades instead of exotic alloys keeps material spend manageable.
Die and Tooling Costs
Tooling non-recurring engineering (NRE) fees range from $2,000 for simple single-stage dies to over $30,000 for complex multi-station progressive dies.
Part Geometry and Manufacturing Complexity
Intricate bends, narrow slots, and deep drawn cups demand additional die stations, increasing tooling cost and press tonnage requirements.
Production Volume and Order Quantity
Larger order batches yield substantial economies of scale by spreading press setup fees over more units.
Tolerance, Inspection and Quality Requirements
Demanding zero-defect CMM reports or sub-0.02 mm tolerances requires frequent tool maintenance and slower press speeds, increasing unit prices.
Surface Treatment and Secondary Processing
Adding electroplating, powder coating, or deburring steps adds processing fees to the final part cost.
How to Reduce Sheet Metal Stamping Costs
To optimize your overall metal stamping cost, standardize hole sizes, maintain generous inside bend radii, and simplify cutouts to cut down on die stations.
Sheet Metal Stamping for OEM and ODM Product Manufacturing
Contract manufacturing partners guide hardware projects smoothly from initial concept sketches to mass production.
From Product Concept to Production-Ready Stamped Parts
Transforming industrial design sketches into production-ready metal parts requires aligning functional specs with press shop capabilities.
Engineering and DFM Support
A dedicated sheet metal stamping DFM review identifies tight radii, unneeded bends, and narrow slots before tool steel is cut.
Prototype and Tooling Development
Prototyping using laser cutting and soft press brakes lets engineers validate fit and form before locking in hard progressive tooling designs.
EVT, DVT and PVT Validation
The path to volume production follows structured verification milestones:
- EVT (Engineering Validation Test): Verifies basic mechanical geometry using prototype soft tools.
- DVT (Design Validation Test): Tests parts off initial hard tooling to confirm functional tolerances and strength.
- PVT (Production Validation Test): Runs hard tooling at full production speeds to validate yield rates and process stability.
Pilot Production and Production Ramp-Up
Low-rate initial production (LRIP) uncovers setup bottlenecks, allowing process refinement before launching full-capacity runs.
Mass Production and Quality Assurance
Continuous inline monitoring and automated vision systems protect part quality across high-volume production shifts.
Supply Chain and Production Management
Integrated contract manufacturing manages raw material coil sourcing, secondary plating, and packaging logistics under one roof.
How to Choose a Sheet Metal Stamping Manufacturer
Partnering with a reliable sheet metal stamping manufacturer ensures consistent quality and on-time delivery across your product lifecycle.
Evaluate Stamping and Tooling Capabilities
Verify press tonnage ranges (from 25 to 800+ tons) and inspect toolroom capabilities to confirm your supplier handles tool builds in-house.
Check Material and Part Size Capabilities
Ensure the factory works with your target material alloys—whether soft aluminum or high-strength stainless steel—at required sheet gauges.
Review Quality Control Processes
Look for essential industrial quality accreditations, such as ISO 9001, IATF 16949 (automotive), or ISO 13485 (medical equipment).
Assess Engineering and DFM Support
Select a partner whose engineering team provides active DFM feedback to optimize your part designs for mass production.
Consider Production Capacity and Scalability
Confirm the shop maintains sufficient press availability to handle unexpected volume surges without production bottlenecks.
Verify OEM/ODM Manufacturing Experience
Working with an experienced sheet metal stamping company grants access to high-tonnage press suites and skilled toolmakers familiar with complex hardware builds. A tier-one metal stamping manufacturer maintains rigorous ISO certifications and robust traceabilities across raw material batches.
Questions to Ask Before Selecting a Stamping Partner
1. Do you design and maintain stamping dies in-house?
2. What are your standard inspection sampling rates (AQL levels)?
3. How do you manage tool wear and maintenance schedules over high-volume runs?
Related: Product Design Explained: How to Turn Your Idea into a Manufacturable Product (2026)
What Information Does a Manufacturer Need for a Sheet Metal Stamping Quote?
Providing complete technical data upfront speeds up quote turnaround times and prevents miscommunication.
2D Drawings and 3D CAD Files
Supply native 3D files (STEP, IGES) alongside 2D PDFs showing critical dimensions, geometric tolerances (GD&T), and key interface points.
Material and Thickness Requirements
Specify exact material grades (e.g., Stainless Steel 304 1/2 Hard) and nominal sheet gauge thickness with allowed tolerances.
Annual and Initial Production Volume
Indicate initial prototype batch quantities along with estimated annual run volumes to determine the right die configuration (stage die vs. progressive die).
Tolerance and Quality Specifications
Highlight tight tolerances, critical fit-to-function callouts, and required inspection levels (e.g., CMM reports, FAIR).
Surface Finish and Secondary Operations
Specify deburring requirements, surface treatments (zinc plating, anodizing, e-coating), and hardware insertion needs.
Packaging and Delivery Requirements
Define packaging standards—such as tape-and-reel for automated surface-mount placement, layered foam trays, or bulk egg-crate cartons.
Ready to Bring Your Product to Life?
Share your product requirements, CAD files, or initial concept with our engineering team.
Why Choose Precintl for OEM & ODM Sheet Metal Stamping
Precintl delivers contract OEM sheet metal stamping tailored to strict brand specifications, bridging the gap between design engineering and mass manufacturing. When starting from a rough product sketch, our ODM sheet metal stamping service takes care of full mechanical architecture, die development, and box-build assembly.
Engineering-to-Mass-Production Support
Our engineering team guides your project through every stage, ensuring smooth transitions from CAD concepts to high-yield mass production.
DFM, Prototyping and Tooling Coordination
We evaluate part geometry early, delivering practical DFM recommendations that streamline die builds and reduce tooling expenses.
Quality Control and Production Validation
With advanced CMM equipment, optical measurement systems, and strict SPC monitoring, we keep production runs strictly within spec.
Scalable Manufacturing for Growing Product Lines
Whether you need initial pilot batches or high-volume continuous production, our scalable press infrastructure adapts to your schedule.
Integrated OEM/ODM Supply Chain Support
From raw coil procurement to secondary plating, assembly, and custom packaging, Precintl manages your complete manufacturing supply chain.
Request a Sheet Metal Stamping Quote
Outsourcing your hardware needs to specialized metal stamping services reduces initial capital risk. Contact our engineering team at Precintl to review your CAD files and receive a competitive quote.
Frequently Asked Questions About Sheet Metal Stamping
What is sheet metal stamping used for?
It is used to transform flat metal sheet stock into functional 3D hardware components—such as brackets, enclosures, clips, connectors, and automotive panels—at high production speeds with high repeatability.
Which metals are best for sheet metal stamping?
Ductile alloys with good elongation properties perform best. Common options include mild carbon steel (SPCC), austenitic stainless steel (304), aluminum (5052), brass, and copper.
Is sheet metal stamping suitable for low-volume production?
For low volumes (under 1,000 pieces), laser cutting combined with press brake forming is usually more cost-effective. However, stage tooling or soft dies make single-operation stamping viable for medium runs.
How much does sheet metal stamping cost?
Unit costs are typically low (often under $1.00 per part for high runs), but upfront tooling costs range from $2,000 to over $30,000 depending on die complexity, stroke count, and material gauge.
How do I choose a sheet metal stamping manufacturer?
Look for a supplier with in-house tooling maintenance, strong DFM support, verified quality accreditations (ISO 9001/IATF 16949), and proven OEM/ODM manufacturing experience in your industry.
Get a Custom Sheet Metal Stamping Solution for Your Product
Ready to turn your engineering drawings into production-ready stamped components? High-precision custom metal stamping requires engineering rigor, robust toolmaking, and dependable quality management.
Share Your Drawings, CAD Files and Production Requirements
Upload your 2D drawings and 3D CAD models (STEP/IGES) along with material specs and annual volume targets.
Get DFM Feedback and Manufacturing Recommendations
Our engineering team will review your design, provide actionable DFM optimization feedback, and deliver a detailed cost quote.
Move From Tooling and Prototyping to Mass Production
Partner with Precintl to move smoothly from initial EVT prototype samples to high-volume production runs. Contact us today to start your custom manufacturing quote.